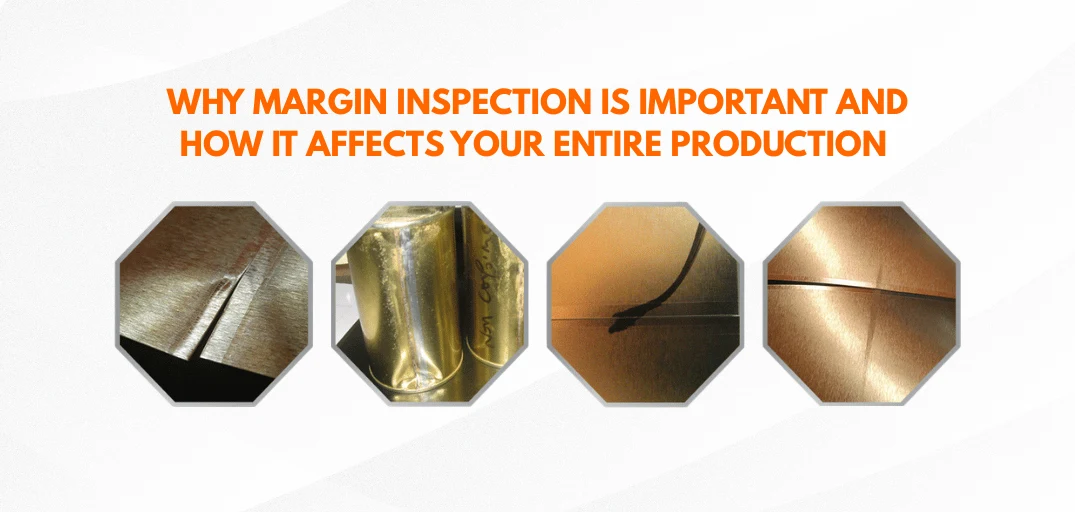
Margin inspection checks the uncoated strips (margins) of a coated sheet before the slitter cuts it and the welder forms it into 3-piece can bodies. This matters because the weld runs along the margin. As a result, a margin that is misaligned, dirty or carrying lacquer leads to broken weld wire, burnt weld rolls, poor welds, leaking cans and unplanned downtime.
Good welding depends on three things:
- The margin sits in the correct position
- The margin is clean and free from contamination
- The welder itself is in sync and in good condition
This article covers the first two: what goes wrong on margins, why it happens, and how the IS610 Plain Margin Inspector catches it before the sheet reaches the welder.
Key takeaways on margin inspection
- The weld on a 3-piece can body runs along the sheet margin, so a misaligned, dirty or lacquered margin directly causes broken weld wire, burnt weld rolls, poor welds and leaking cans.
- The three most common margin defects are misaligned margins, dirty margins (grease, oven tar, rust) and lacquer on the margins (feathering).
- Margin inspection on the slitter catches these defects before the welder. The IS610 Plain Margin Inspector detects any type of lacquer, including clear lacquers, plus grease, oil, rust and water marks, with a response time of 4 milliseconds or better.
Margin defects at a glance
| Defect | Typical cause | Result at the welder |
|---|---|---|
| Misaligned margins | Sheets moved sideways or skewed in the coater or slitter | Lacquer on the margin |
| Dirty margins | Grease, oven tar, rust, water marks or fingerprints | Weld wire breakage and poor weld quality |
| Lacquer on margins (feathering) | Uncleaned roller grooves, high lacquer viscosity or lacquer starvation | Burnt weld rolls and weld wire breakage |
Why is margin contamination a problem?
Margin contamination is one of the leading causes of unplanned downtime in welded can production. For example, a contaminated margin can break your tooling or cause a bad weld that makes the can leak. The most common contaminants are:
- Lacquer splashes
- Water splashes
- Fingerprints
- Dust
In addition, uninspected margins can carry defects from earlier in the line. Here are the three most common.
What are the most common margin defects?
1. Misaligned margins
Misaligned margins come from sheets that have moved sideways or skewed in the coater or in the slitter. Fortunately, you can monitor sheet skew at the coater with the IS416 Sheet Skew Measurement System.
Result: lacquer ends up on the margins.
2. Dirty margins
Margins get dirty when contaminants such as grease, rust, water marks or fingerprints get onto them.
- Grease from equipment. Every bearing runs on grease, so grease can drip or spill into a machine and onto the plates. This is rare, but you should always prevent it.
- Tar from the ovens. More often, the “grease” is actually tar from the curing ovens. As sheets pass through the ovens, volatile organic substances evaporate from the lacquer. Then they condense in colder parts of the oven and slowly burn into a sticky tar. Eventually, when enough builds up, it drops back onto the sheets, and it can land right on the margin.
- Rust. Margins can also rust when tinplate sits in adverse atmospheric conditions.
Result: contaminants cause weld wire breakage and poor weld quality.
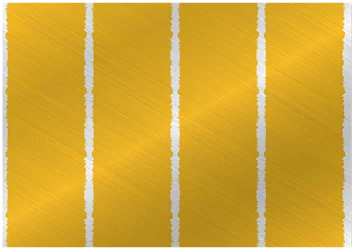
3. Lacquer on margins (feathering)
If nobody cleans the grooves in the coater rollers, lacquer can get onto the margins. As a result, feathering appears along the sheet margins:
In addition, two lacquer supply problems can put lacquer on the margins:
- High lacquer viscosity. Either the lacquer is fine but too cold (cold lacquer becomes more and more viscous), or its solid content is too high. Every lacquer is a resin (the solid) dissolved in a solvent. In other words, with a fixed amount of solvent, the more resin you dissolve, the higher the viscosity.
- Lacquer starvation. The coater takes its lacquer from a small day tank at the side of the machine, which feeds the rollers. The line operator keeps the day tank at a working level by pumping lacquer in from the drum. Some factories automate this. However, if the day tank calls for more lacquer and the drum is empty, the coater runs out of coating.
Result: if lacquer is present on one margin, it is likely present on the other margins too. Lacquer on margins leads to burnt weld rolls and weld wire breakage.
How does the IS610 help with margin inspection?
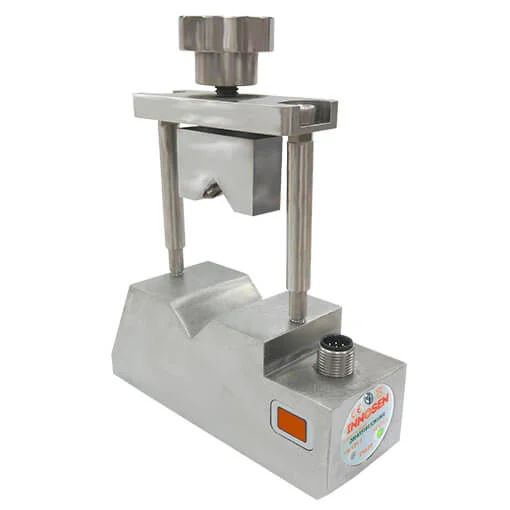
The IS610 Plain Margin Inspector detects lacquer and other contaminants on the sheet margins before they can damage equipment, cause prolonged downtime, reduce productivity, break weld wire, burn weld rolls or lower weld quality.
On a typical sheet with four margins, one sensor detects up to 80% of the defects from coating to curing, according to customer feedback, protecting your welder from damage and downtime.
How does the IS610 detect margin defects?
The IS610 sits on the slitter, above the sheet and close to the cutting roll. It inspects a strip approximately 3 mm wide at the center of the margin and sends a good/bad output pulse to the slitter. Its response time is 4 milliseconds or better. It detects lacquer down to 2 g/m² and rejects defects from 2 mm in length, depending on the lacquer, line speed and other factors. Because it is auto-learning and self-calibrating, operators do not need to recalibrate it between jobs, and it needs no external controller.
Which margins can the IS610 inspect?
Innosen has tested the IS610 on the inner margins of the sheet only. Outer margins take the first impact from the side lays as the sheet enters the cutter roller, so they are more prone to vibration and fluctuation. Larger cans mean fewer inner margins per sheet. In that case, you can still install sensors on the outer margins to inspect every margin, although Innosen cannot guarantee reliable operation there.
Key features of the IS610
- Auto-learning, self-calibrating sensor
- Clip-on alignment tool for fast, easy sensor alignment
- Easy Fit housing designed to sit very close to the cutter blades
- Heartbeat signal so you know the sensor is still working
- Works on clear lacquers and detects fingerprints
- Configurable output pulse period to match the slitter’s input timing requirements
- Special mounting kit for easy installation and adjustment, able to hold several sensors
- Stainless steel housing, resistant to shock, vibration and humidity
- Adapts to any line speed
Protect your welder with the IS610
Catch lacquer and contamination on sheet margins before they reach the welder.
FAQs about margin inspection
What is margin inspection in canmaking?
Margin inspection checks the uncoated strips of a coated sheet for lacquer, contamination and misalignment. The welder joins the can body along these strips, so the check happens before slitting and welding.
What contaminates sheet margins?
Common contaminants are lacquer and water splashes, fingerprints, dust, grease from equipment, tar dropping from the curing ovens, and rust on tinplate exposed to adverse atmospheric conditions.
What happens if lacquer gets on the weld margin?
Lacquer on the margin leads to burnt weld rolls, broken weld wire and poor welds. Consequently, cans can leak.
What causes feathering on sheet margins?
Feathering happens when lacquer spreads onto the margin, usually because nobody cleaned the roller grooves or the lacquer is too viscous (too cold or too high in solids).
Can the IS610 detect clear lacquer?
Yes. The IS610 detects any type of lacquer on the margin, including clear lacquers and varnishes. It also detects grease, oil, rust and water marks.
Where is the IS610 installed?
On the slitter, above the sheet and close to the cutting roll. One mounting kit can hold several sensors, so you can inspect several margins.
How many IS610 sensors do I need?
On a typical four-margin sheet, one IS610 sensor detects up to 80% of the defects from coating to curing, according to customer feedback. You can add more sensors; however, Innosen has tested the IS610 on inner margins only.